Signage factory acceptance testing should cover documents, dimensions, materials, welds and coatings, electrical safety, illumination, LED performance, control systems, continuous operation, spares and a closed punch list, all before the sign leaves the factory.
Skip this step and any fit-up gap, dead pixel, or wiring fault becomes a shipping-container problem instead of a factory-floor problem. Fixing it after export costs far more in freight, time and reputation than catching it before packing.
Here at Hicen, this is the stage where a sign either earns its shipment or gets held back, and buyers should know exactly what that process looks like before they sign off on a supplier.
Approve the FAT Procedure Before Production Starts
Agree on the test scope, the acceptance criteria, and who signs off on what, before fabrication begins, not the week before shipping. A FAT procedure written after the sign is built tends to fit the sign rather than protect the buyer.
Map every project requirement to a specific FAT record. If your contract calls for a certain paint finish, a certain wind rating, or a certain LED brightness, each one needs a named test and a named pass criteria in the procedure. Vague language like “tested for quality” gives you nothing to hold a supplier to.
Decide your witness points early too. You do not need to fly someone to the factory for every test, but you should know in advance which milestones you will review in person, by video call, or through documented reports.
Verify Structure and Appearance Against Real Tolerances
This stage catches the defects a photo will not show you later. Structural fit-up, weld quality and surface finish need checking against numbers, not general impressions.
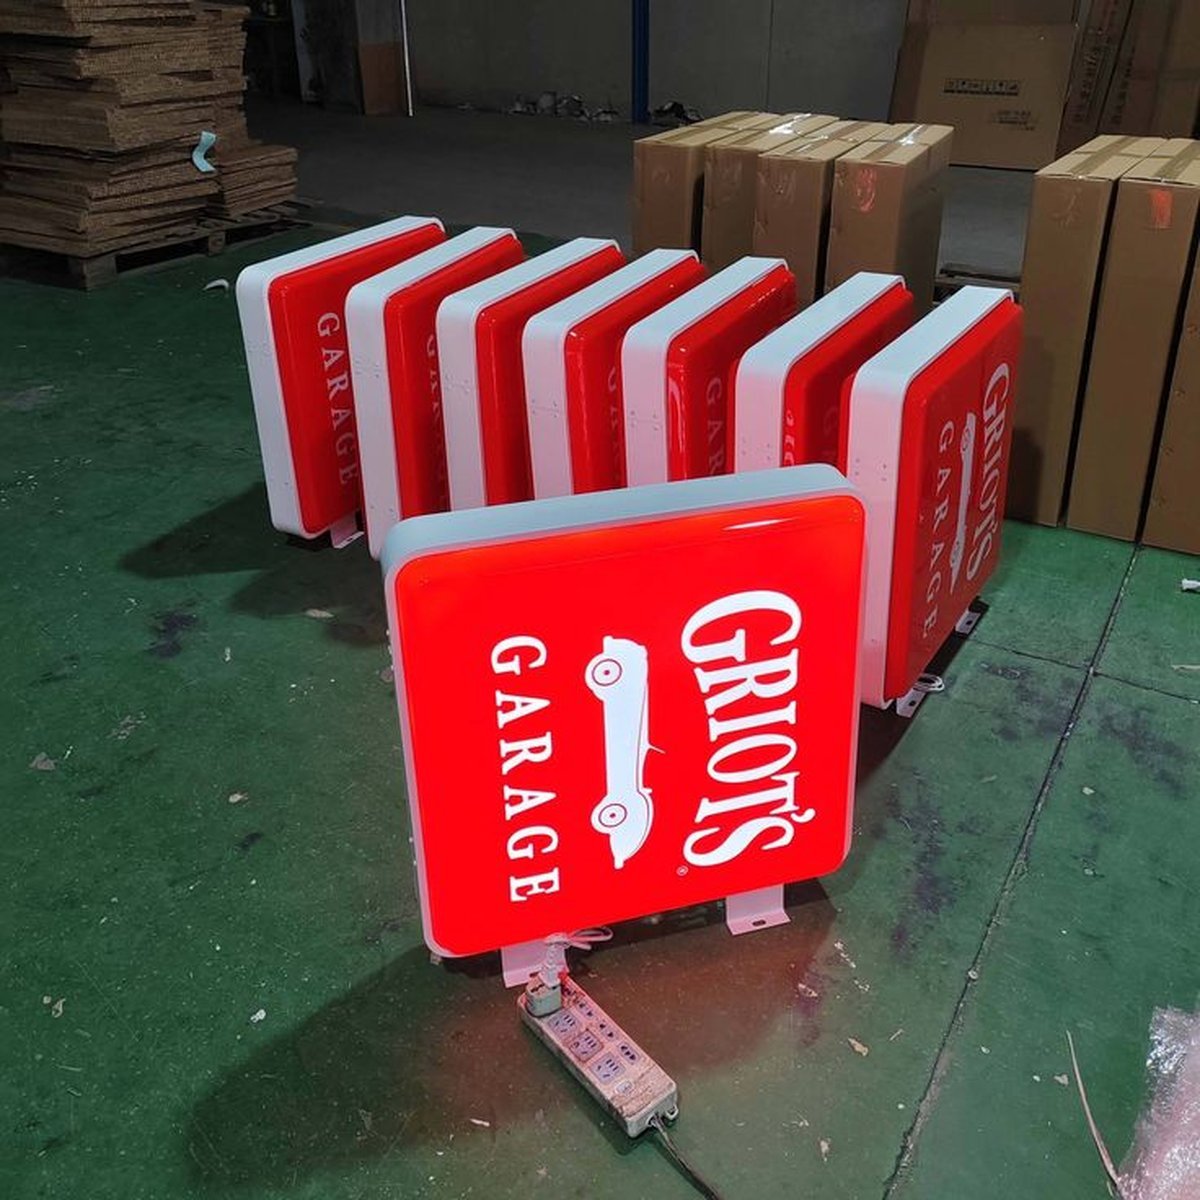
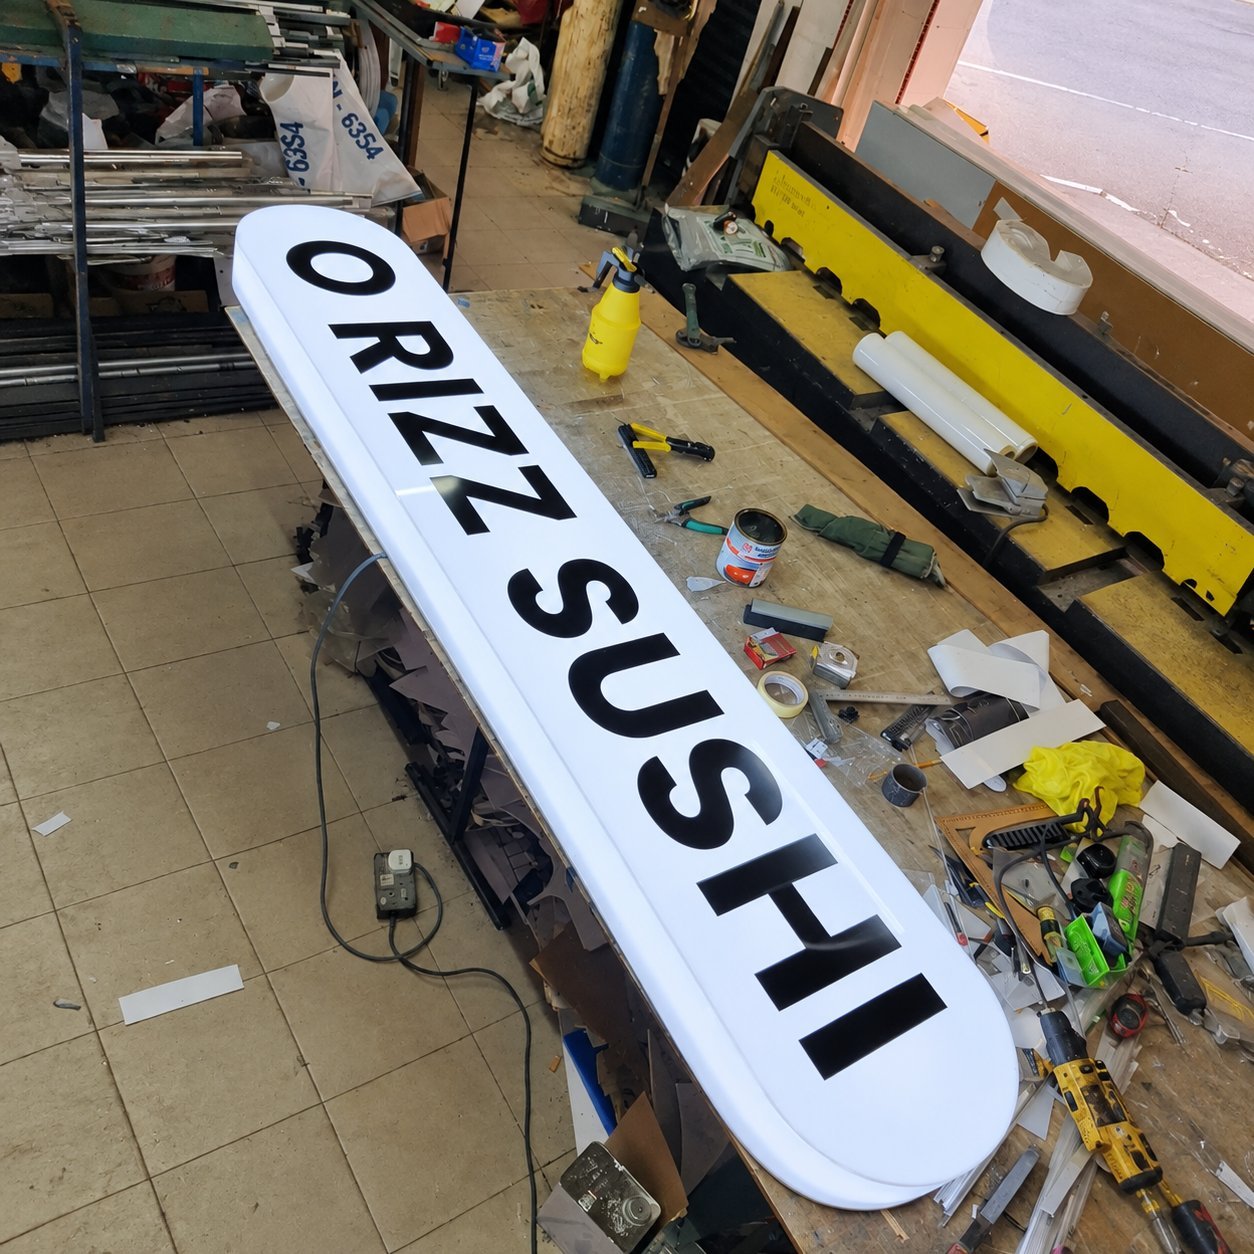
At Hicen, laser-cut components are held to a dimensional tolerance within 0.5 mm, with clean edges free of burrs. Welds are checked for full penetration, no cold joints, and a fully polished, flat finish at every weld spot. These are not abstract targets. A module that is out of tolerance at this stage is a module that will not align cleanly with its neighbors once it is mounted on site.
Surface materials get checked too. Every batch of outdoor fluorocarbon paint, powder coating and plating material gets verified before it goes onto a sign. Metal sheet stock, steel, aluminum, stainless, brass, copper, gets inspected for correct thickness and a flat surface free of scratches or rust before it enters production.
Ask any supplier what they check at incoming material stage. That answer tells you a lot about what happens downstream.
| FAT Check | Acceptance / Test | Hicen Process |
|---|---|---|
| Dimensional tolerance | Within 0.5 mm | Laser-cut parts verified against drawing before assembly |
| Weld condition | Full penetration, no cold joints | Polished flat finish at every weld spot |
| Material condition | No scratches, no rust, correct thickness | Incoming stock inspection for steel / aluminum / stainless / brass / copper |
| Surface finish | Batch-verified fluorocarbon paint, powder coat, plating | Each batch approved before it enters production |
| Finished sign aging | 48 hours continuous power-on | Burn-in surfaces early LED, driver and flicker failures |
| Power supply load test | 4 consecutive hours under full load | Temperature and voltage stability monitored |
| Water spray test | 15 – 30 minutes | Sprayed across glue joints, wire outlets, panel bonding points |
| LED uniformity | Even arrangement, no dark spots or bright dots | Channel letter / light box face inspection |
| Grounding / electrical safety | Insulation, grounding, circuit function, protection devices | Verified before any longer powered test |
| Waterproofing | Outdoor-rated seals at LED assembly | Filling-glue seal on illuminated components |
| Large LED display burn-in | 24 – 72 hours typical | Confirm duration and defect thresholds with the display manufacturer |
Note: large-format digital LED display faces typically ship from a specialized display partner rather than a channel-letter or light-box factory, so their burn-in duration and dead-pixel thresholds vary by manufacturer. Confirm the exact scope with whichever factory builds that specific component.
Test LED and Electrical Functions Before Sign-Off
Electrical safety testing comes first here: insulation, grounding, circuit function and protection devices all need verification before anything gets powered up for a longer test.
For the illuminated components Hicen manufactures directly, channel letters, light boxes and halo-lit signage, LED assembly is checked for even arrangement with no dark spots or bright dots, then sealed with filling glue to meet outdoor waterproof standards.
Every finished sign then runs a 48-hour continuous power-on aging test. That is long enough to surface early LED failures, flickering or driver faults that a five-minute check would miss entirely. Power supplies get their own test too, running under full load for four consecutive hours while temperature and voltage stability are monitored.
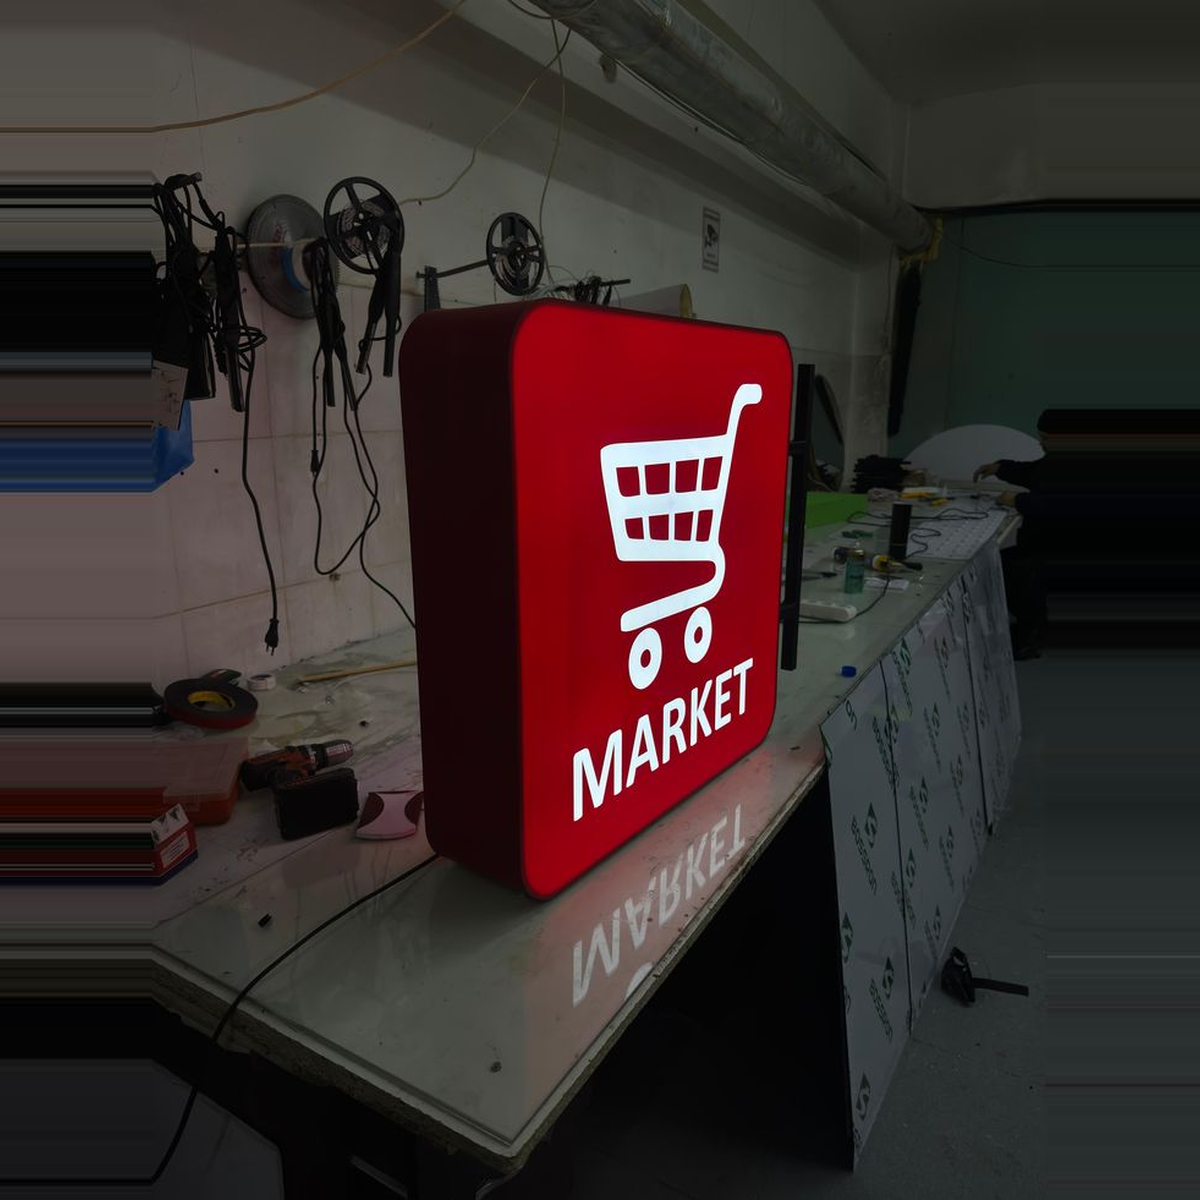
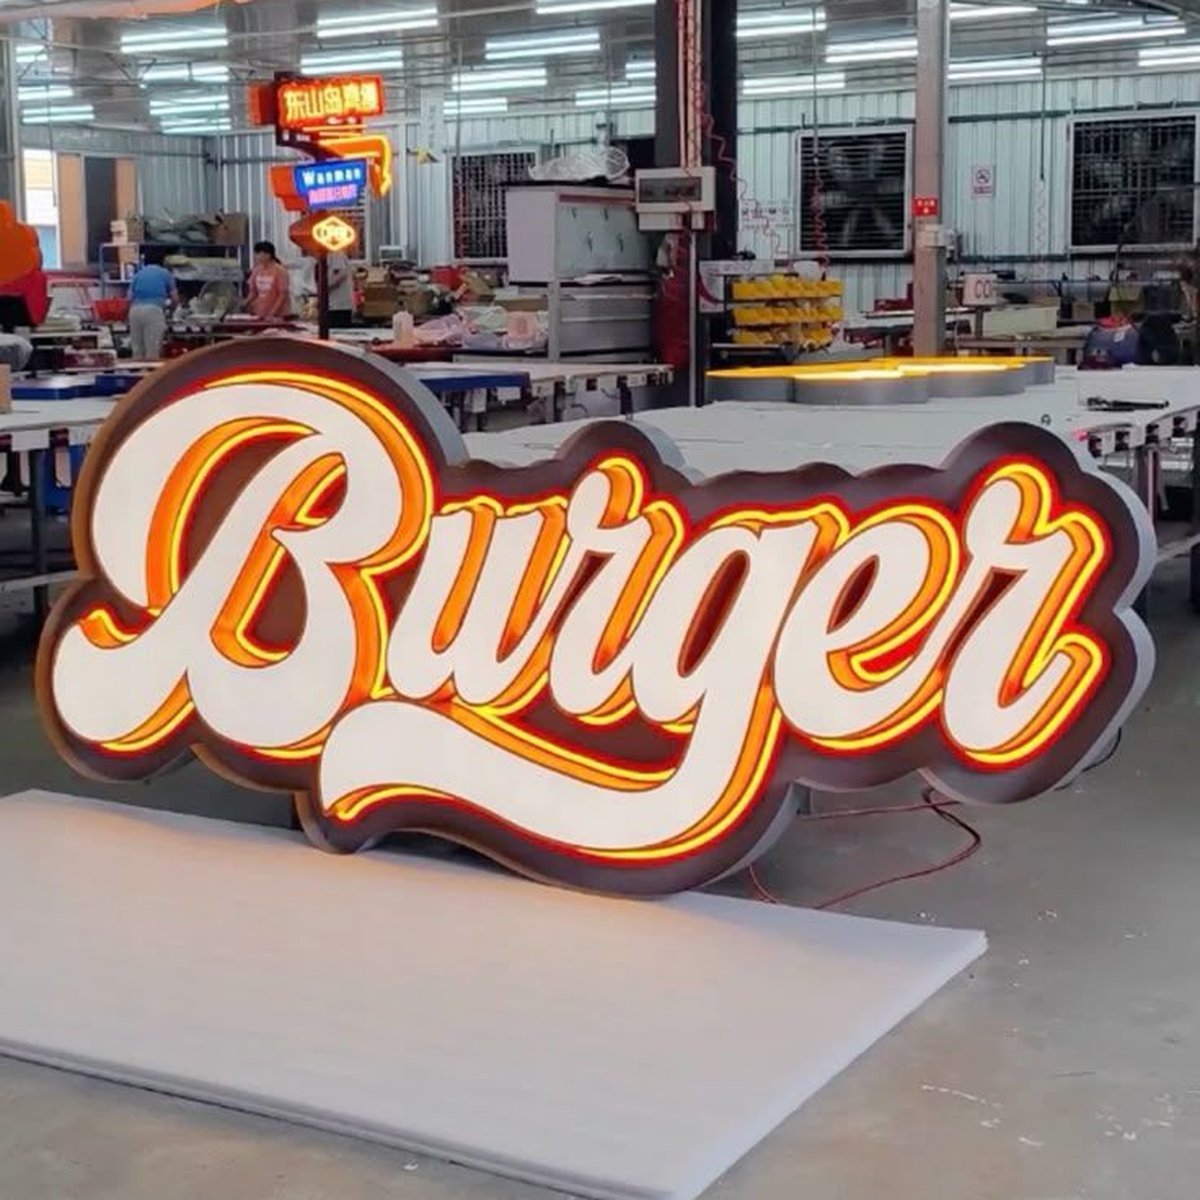
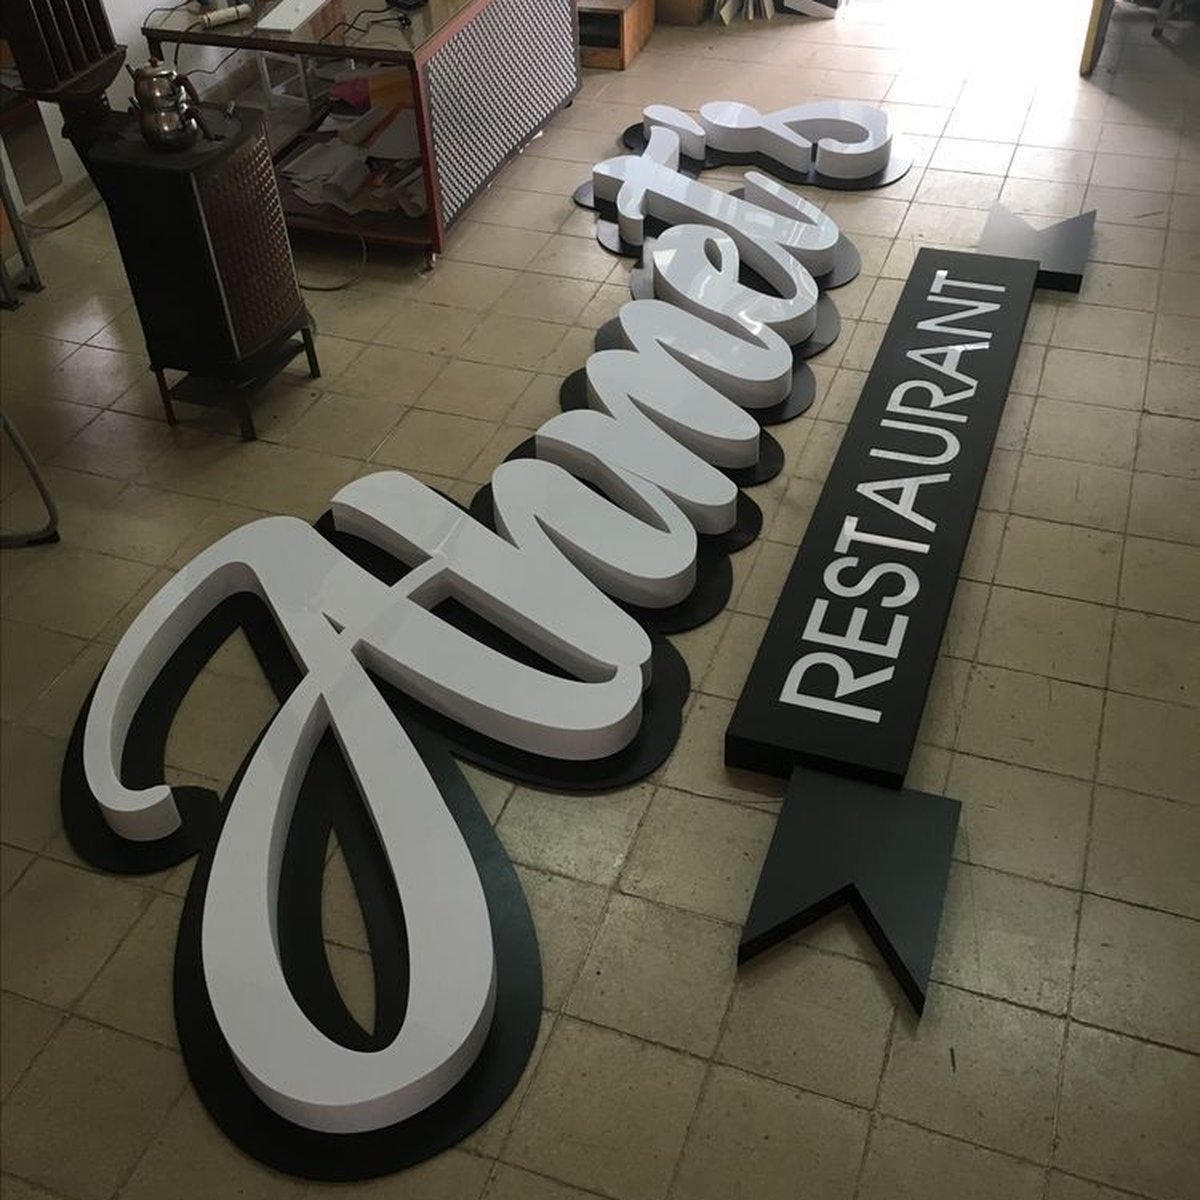
Waterproofing gets tested directly rather than assumed. Inspectors spray water evenly across glue joints, wire outlets and panel bonding points for 15 to 30 minutes, then open the unit to check for seepage.
If your project includes a large-format digital LED display face, that component typically ships from a specialized display partner rather than from a channel-letter or light-box factory, so its FAT looks a little different.
Ask for dead-pixel counts, brightness and color calibration records, content playback verification and a burn-in period, ideally 24 to 72 hours of continuous operation, before it is accepted. Confirm this scope with whichever factory actually builds that component, since burn-in duration and defect thresholds vary by manufacturer and are not a fixed industry number.
Build a Traceable Handover Package Before Packing
A test that is not documented is a test you cannot prove happened. Every stage needs a record: signed inspection sheets, photos, video where practical, the instruments used, and calibration details for anything measured.
Hicen runs this as a five-step system: incoming material inspection, in-process production patrol, semi-finished product sampling, comprehensive finished-product inspection covering aging, waterproofing, dimensions and appearance, then a final recheck before packing. Complete packing lists and QC checklists ship with every order, so what left the factory is documented, not just assumed.
Close every nonconformity before the sign gets packed, not after. An item marked “accept with corrective action” that never gets a documented fix is a defect waiting to surface on your job site instead of your factory floor.
| Record | What the Buyer Should Receive |
|---|---|
| Inspection sheets | Signed FAT / QC records for every stage |
| Photos | Visual evidence of finish, fit-up, illumination |
| Video | Witness / testing evidence where practical |
| Measurement records | Instrument readings and test results |
| Calibration details | Traceability for any instrument used in measurement |
| Packing list | Full shipment contents |
| QC checklist | Final inspection status at packing |
| Punch list | Closed and signed off before packing |
How Hicen Runs FAT on a Complete Sign Package
Hicen applies this same five-step process to every illuminated sign we manufacture. We coordinate the same discipline with LED display partners when a project includes a large-format digital face as part of a turnkey project.
Our full quality control process and manufacturing process documentation are available for your review. Our certifications give your team a starting point for setting acceptance criteria.
If you are sourcing a complete outdoor sign package or comparing suppliers for a larger sign project, ask each one for their actual FAT numbers, not just a claim that testing happens. The gap between those two answers tells you most of what you need to know.
Explore Hicen Signage Solutions by Industry
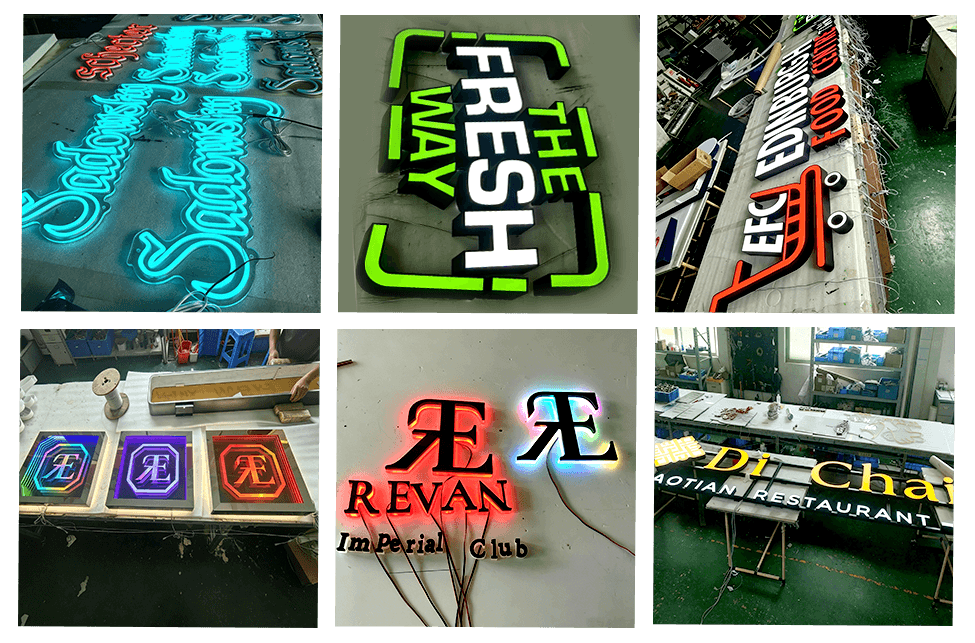
Retail, shopping malls, hotels, restaurants, scenic spots, airports and transit hubs — see how Hicen structures a complete sign package, from illuminated branding to large-format digital displays, with FAT built into every step.
View Industry SolutionsFrequently Asked Questions
Must the owner witness FAT in person?
No, though it helps on larger or higher-risk projects. Many buyers review test records, photos and video documentation instead of traveling to the factory, and reserve in-person or video witnessing for specific milestones that matter most to them. Tell us which stages matter to your project and we will build the witness plan around that.
How long should LED display burn-in testing last?
For illuminated signage components, a 48-hour continuous power-on test is a solid baseline that reveals most early failures. Large-format LED display faces from a specialized partner often run 24 to 72 hours, depending on the manufacturer’s own standard. There is no single number that applies everywhere, so confirm the exact duration with whichever factory builds that specific component.
Can FAT replace site commissioning?
No. FAT confirms the sign works correctly in factory conditions before it ships. Site commissioning confirms it still works after transport, installation and connection to your actual site power and structure. Both matter, and skipping either one leaves a real gap in your quality process.
Get a Project-Specific FAT Checklist
Send us your sign type, project specifications, acceptance requirements and any witness or testing requirements, and we will return a factory acceptance test checklist mapped to your actual signage package, covering every stage from incoming materials through the final pre-packing recheck.
Request a FAT Checklist